When to use this guide
Use it for aggressive outdoor steel, structural parts, energy-storage cabinets and machinery where an EZ or E primer sits under a P480, P720 or P1680 topcoat.
What you need
- Primer (E or EZ) and topcoat (P series) samples in the target colour
- Production-pretreated panels or parts
- Your cure profile for both coats
- The test programme your customer or standard requires
Steps
Fix the system and the target
Write down primer, topcoat, film thickness for each coat and the result the specification requires.
Prepare panels on your line
Use production pretreatment. TDS values come from phosphated steel; your line sets the real ceiling for adhesion and corrosion life.
Apply and cure as in production
Apply the primer, then the topcoat, using the cure schedule you will really run, and record the object-temperature profile.
Test inter-coat adhesion first
Cross-cut (ISO 2409), impact (ISO 6272-2) and bend (ISO 1519) on the two-coat film reveal cure mismatch early.
Run humidity and salt spray on the system
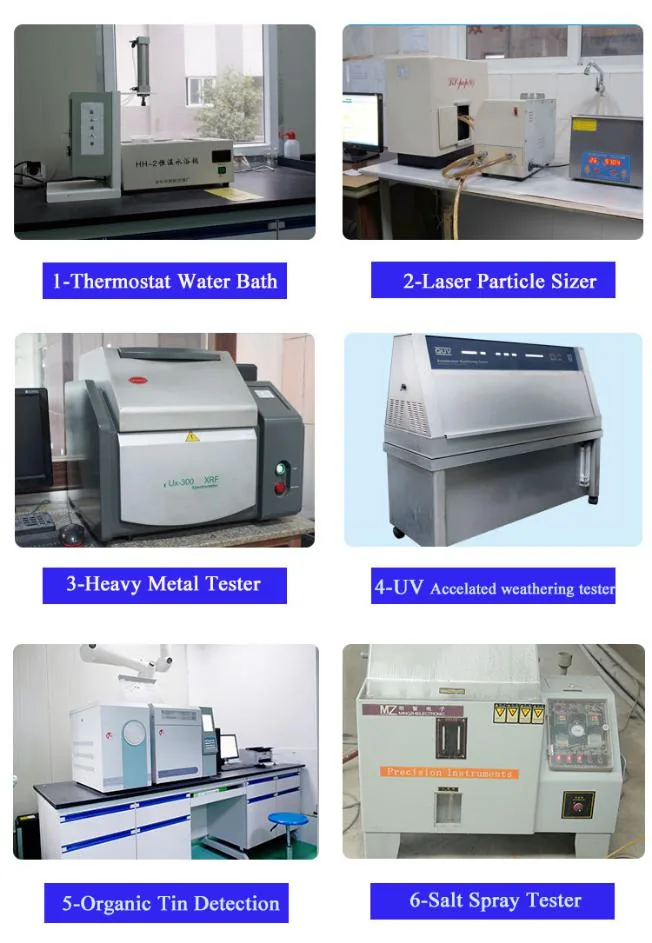
Test the combined system to ISO 6270-1 and ISO 9227. WANAN’s CNAS-accredited laboratory can run these during qualification.
Freeze the parameters
Record film thicknesses, cure profile and batch numbers in the qualification file before release.
Key values
| Item | Value | Source |
|---|---|---|
| Primer options | E (1440 h) or EZ zinc-rich (≥ 2000 h) single-coat salt spray | Series TDS |
| Topcoat options | P480 / P720 / P1680 | Series TDS |
| Rule | System values are tested, never added | Powder coating 101 |
| Laboratory | CNAS L15415, ISO/IEC 17025:2017 | Certifications |
Common mistakes
- Quoting the EZ primer’s ≥ 2000 h as the system result
- Curing the primer differently from the production plan
- Skipping inter-coat adhesion and going straight to salt spray
- Changing either powder after qualification without re-testing
Related
- EZ zinc-rich epoxy primer
- P720 weather-resistant polyester
- Laboratory and test methods
- All how-to guides
Published 7 October 2026 by the WANAN technical team. Figures are taken from WANAN technical data sheets and the pages linked above.